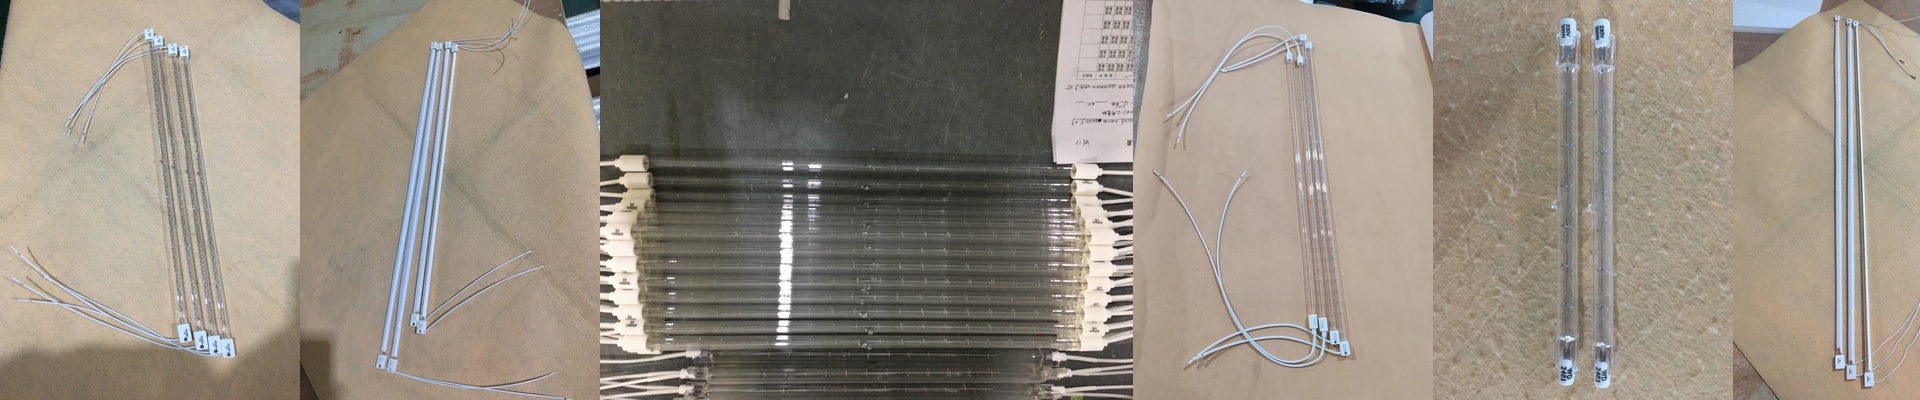

Getting Your Alloy Wheels to Cure Right (Without the Warp)
Curing powder coatings on alloy wheels is a bit of a balancing act. You need enough heat to make the coating flow and lock in, but if you overdo it, you risk warping the metal. That’s why we don’t bother heating up a massive oven volume. It’s a waste of time and money. Instead, we use shortwave infrared lamps that go straight for the metal, hitting your target temperature fast.
How the Tech Actually Works
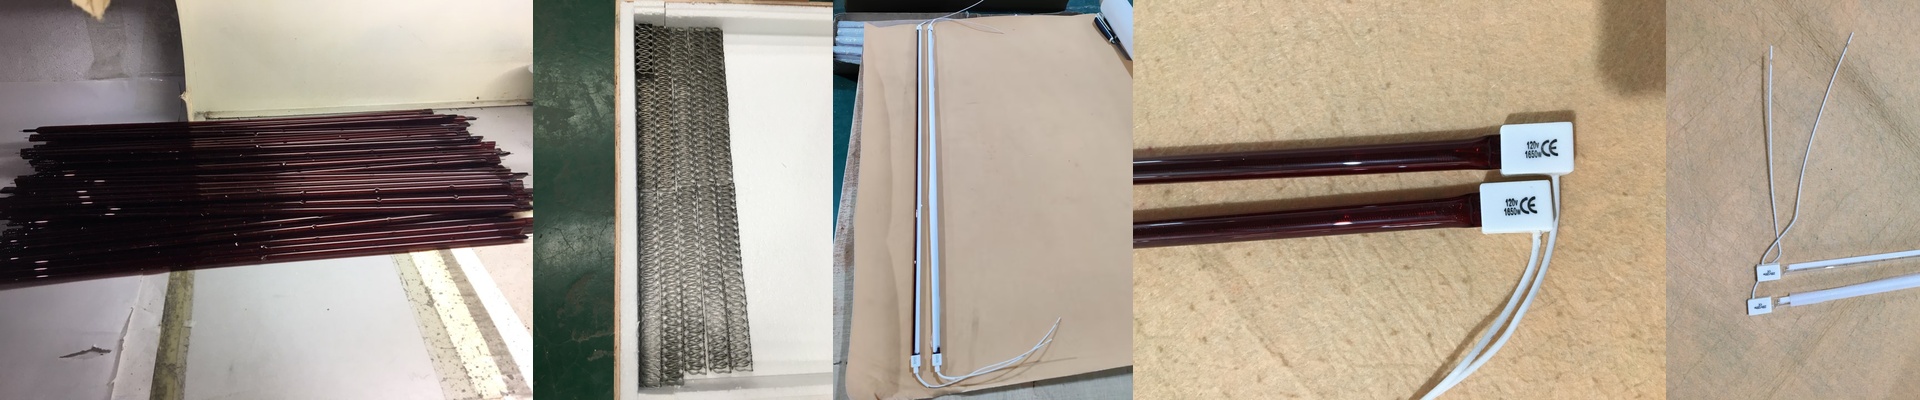
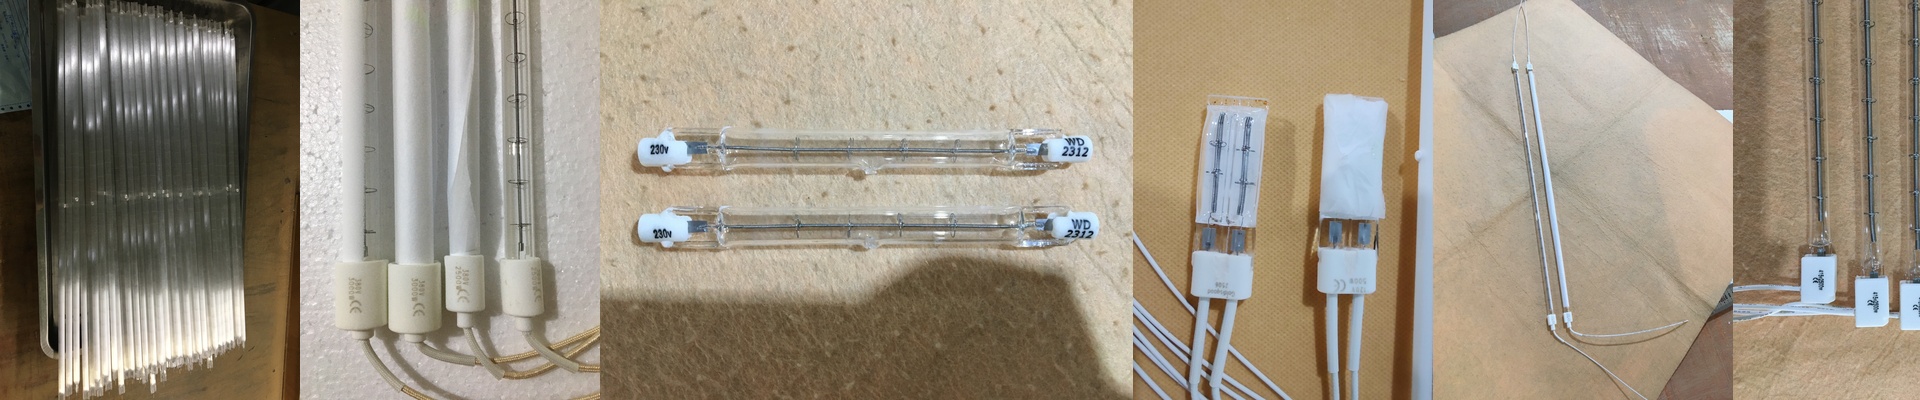
We stick with shortwave radiation for wheels. These lamps run hotter than the medium-wave stuff, which means the energy actually punches through the coating to heat the aluminum itself. To make sure nothing gets blocked, we use high-purity quartz glass. Now, here is the catch: if you run these at full blast, the thermal response is instant. It’s impressive, but it puts a serious strain on your power supply. Just make sure your electrical panels can handle that initial surge when you flip the switch, or you’ll be dealing with tripped breakers.
The Nitty-Gritty of the Build
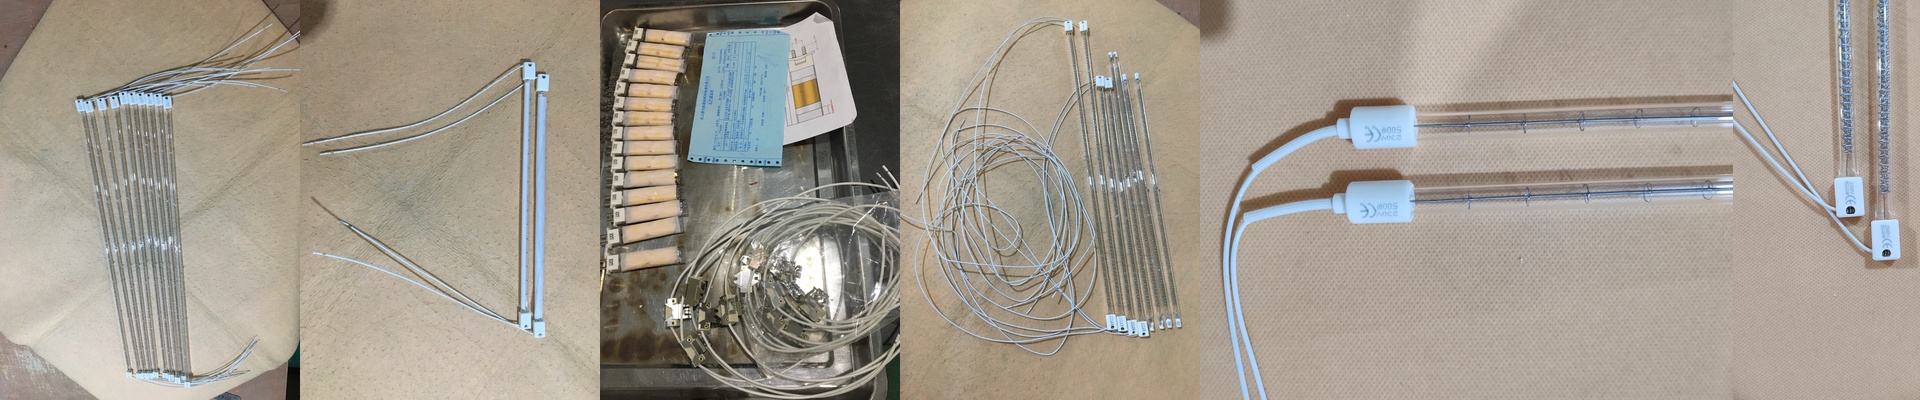
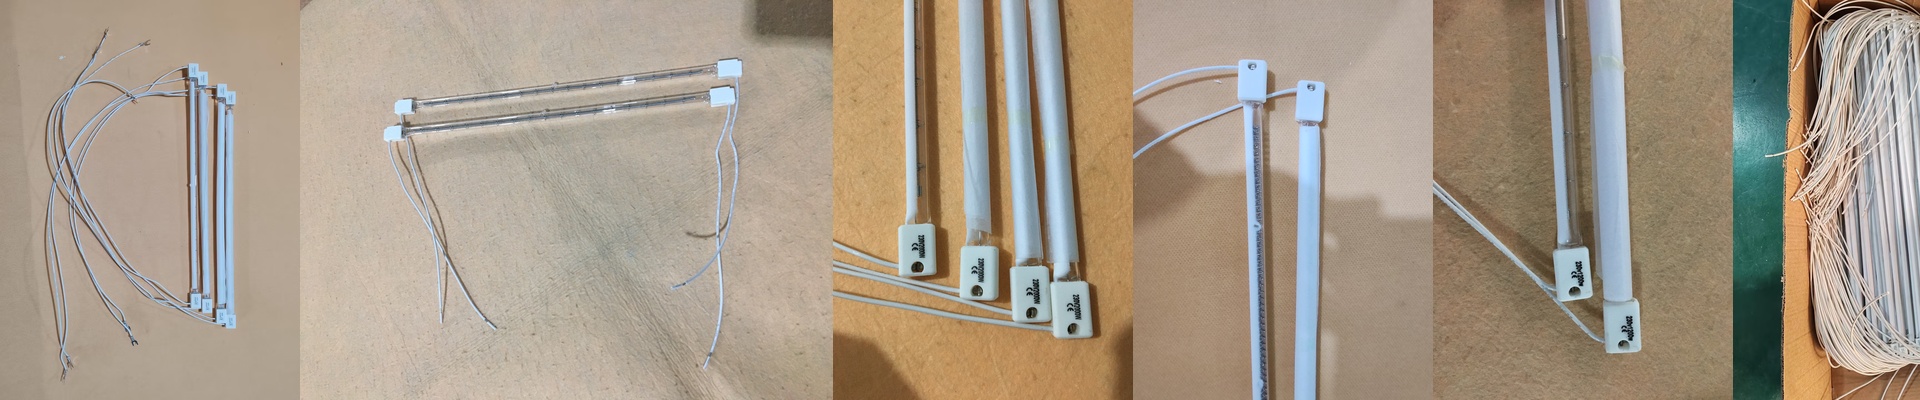
We use heavy-duty filaments because we know these things get cycled on and off all day. Depending on your rack, we use R7s or SK15 connectors. We chose those specifically so that when a tube eventually burns out, you can just pop a new one in and get back to work. We also add a selective coating to the quartz. Think of it as a filter. It stops the energy from just bouncing off the shiny metal wheel and forces it into the paint where it belongs.
Making it Work on Your Floor
Getting these onto a conveyor system is all about the spacing. If you mount them too close? You’ll scorch the coating. Too far? You’re just standing around waiting for the cure to finish. The best way to handle this is to pair the lamps with a closed-loop PID controller and an infrared pyrometer. It basically acts as a set of eyes, watching the actual surface temperature of the wheel and tweaking the power in real-time. It takes the guesswork out of it, so you don’t have to worry about overheating your parts.